Polyethylene Water Tanks Introduction (Highlighting the 1960s Heritage)
Neama Polyethylene Water Tanks: Over 60 Years of Heritage Delivering Advanced Water Storage and Thermal Insulation
Since its initial inception in the 1960s in Kuwait, Neama Group has established a foundational legacy of manufacturing reliability and engineering excellence across the construction sector. Capitalizing on more than six decades of industrial mastery and continuous innovation, Neama delivers its next-generation Polyethylene (PE) water tanks, specifically engineered to outperform the extreme climatic conditions of the Arabian Gulf and safeguard drinking water quality year-round.
Comprehensive solutions for water storage and treatment that meet the highest global standards and are certified by international drinking water tests.
Multi-Layer Polyethylene Water Tanks (PE Systems)
(PE Water Tanks)
Engineered to endure the demanding climate of the Gulf, Neama polyethylene water tanks represent the pinnacle of modern rotational molding technology. Produced using virgin, food-grade Linear Low-Density Polyethylene (LLDPE), each tank features a seamless, uniform body with consistent wall thickness to ensure maximum structural integrity and eliminate stress points.
Available in both standard Vertical and space-saving Short Vertical designs, Neama PE tanks offer fully customizable multi-layer configurations ranging from two up to six specialized functional layers tailored to customer specifications:
- Automated Rotational Molding: Ensures a seamless single-piece structure free of weak joints.
- Advanced Multi-Layer Thermal Defense: Incorporates high-density thermal foam and nitrogen-infused barriers to maintain balanced water temperatures during extreme summer heat.
- Integrated Solid Brass Inserts: Equipped with factory-molded solid brass internal and external fittings for permanent leak prevention.
- Quality Certifications: Manufactured under strict ISO 9001:2015, ISO 14001:2015, and ISO 45001:2018 standards, meeting all approved ministerial specifications in the State of Kuwait.

Approved technical specifications:
Approved Price List for Polyethylene Tanks (Official Price List)
No
|
Item Description
|
Selling Price (KWD)
|
1 |
PE Water Tank - 3 Layers - 500 Gallons
| 85 |
2 |
PE Water Tank - 4 Layers - 500 Gallons
| 110 |
3 |
PE Water Tank - 3 Layers - 750 Gallons
| 100 |
4 |
PE Water Tank - 4 Layers - 750 Gallons
| 140 |
5 |
PE Water Tank - 3 Layers - 1000 Gallons
| 120 |
6 |
PE Water Tank - 4 Layers - 1000 Gallons
| 155 |
7 |
PE Water Tank - 5 Layers - 1000 Gallons
| 175 |
8 |
PE Water Tank - 3 Layers - 1200 Gallons
| 140 |
9 |
PE Water Tank - 4 Layers - 1200 Gallons
| 180 |
10 |
PE Water Tank - 5 Layers - 1200 Gallons
| 200 |
11 |
PE Water Tank - 3 Layers - 1500 Gallons
| 180 |
12 |
PE Water Tank - 4 Layers - 1500 Gallons
| 220 |
13 |
PE Water Tank - 5 Layers - 1500 Gallons
| 240 |
14 |
PE Water Tank - 3 Layers - 2000 Gallons
| 220 |
15 |
PE Water Tank - 4 Layers - 2000 Gallons
| 280 |


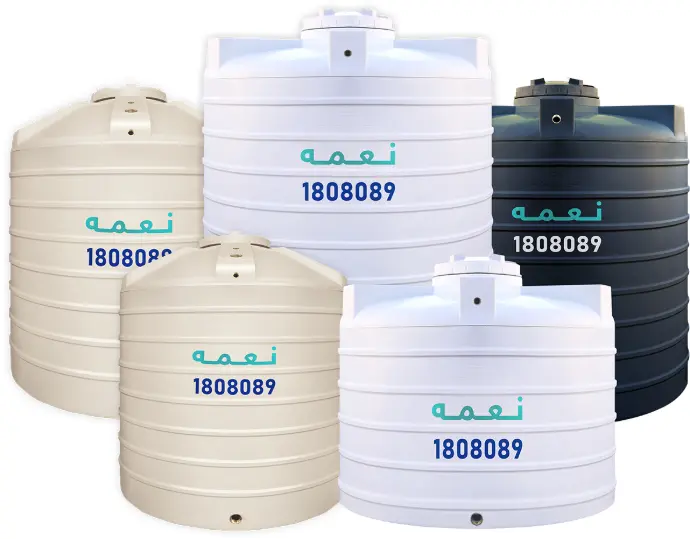
Neama Group manufactures high-density polyethylene water tanks engineered specifically to withstand the harsh Middle Eastern climate. Produced from pure, virgin food-grade LLDPE using advanced rotational molding technology, the seamless body structure is available in configurations ranging from two to six specialized functional layers:
- Protective Outer Shield: Infused with concentrated UV stabilizers to prevent structural weathering, thermal cracking, and color fading under direct sunlight.
- Advanced Thermal Insulation: High-density expanded foam and nitrogen-infused cellular layers work together to insulate stored water against scorching summer heat, keeping it refreshingly cool.
- 100% Light-Blocking Core: A specialized carbon-black barrier eliminates light penetration entirely, halting photosynthesis and preventing bacterial and algal colonization.
- Ultra-Smooth Food-Grade Interior: A pure white, glass-smooth contact surface that prevents mineral sediment adherence, eliminates microbial contamination, and facilitates effortless cleaning.
All tanks feature factory-embedded, solid brass inlet and outlet fittings to ensure leak-free plumbing connections and reliable service for up to 20 years.
Neama Modular GRP Panel Tanks: Six Decades of Industrial Heritage Powering Next-Generation Heavy-Duty Water Storage
Building upon an enduring manufacturing legacy established in Kuwait during the 1960s, Neama Group continues to advance regional water infrastructure with its premier modular GRP panel tanks. Combining over sixty years of industrial leadership with state-of-the-art SMC Hot Press compression technology reaching up to 2,000 tons, Neama delivers engineered storage systems built to conquer the extreme ambient and water temperatures of the Arabian Gulf.
Backed by elite international drinking water certifications—including the UK’s WRAS approval (No. 250555024) and NSF/ANSI 61—our modular systems feature zero residual styrene and innovative external bracing that eliminates all metallic contact with stored water, delivering uncompromising water purity, seismic resilience, and heavy-duty structural integrity for major national and commercial projects.

GRP water tanks made using the Hot Press method are considered the best in the world in terms of quality, efficiency, and lifespan compared to other traditional tanks such as steel, concrete, and plastic tanks, as well as other GRP tanks. Therefore, Neama's GRP tanks are distinguished by international specifications and high quality, produced with the latest machines and equipment. They are assembled pieces available in various sizes, starting from 1000 liters to any required size, with a height of up to five meters.

Neama continues to provide innovative and sustainable solutions to meet the diverse needs of its customers. By offering GRP water tanks in various sizes, the company ensures the highest levels of satisfaction and quality. Whether you need a small tank for residential use or a larger one for industrial applications, we have the perfect solution for you. Our tanks are available in sizes starting from 500 liters, ensuring that you get the right capacity for your specific requirements. Trust Neama to provide reliable and high-quality water storage solutions.

Reliable Water Storage Solutio
Central System Components:
Stainless Steel Booster Pump: Equipped with an automatic device.
Three-Stage Jumbo Filter: Ensures water purity.
Two American Heaters: For efficient heating.
Return Pump: Ensures the circulation of hot water.
Piping Network: For system assembly and operation.
Galvanized Base: Provides sturdy support.
Custom Underground Fiberglass (FRP) Tanks: Over 60 Years of Engineering Mastery in Heavy-Duty Liquid Storage
Carrying forward an industrial legacy rooted in Kuwait since the 1960s, Neama Group manufactures high-performance custom-engineered fiberglass (FRP/GRP) tanks designed to meet the most critical storage demands. Built with seamless, one-piece cylindrical construction for maximum structural load-bearing under soil and hydrostatic pressure, our custom solutions span from 2,000 liters up to heavy-duty industrial capacities of 200,000 liters.
Engineered in single-wall and double-wall configurations to international ISO standards, Neama underground tanks offer tailored, high-grade resin matrices that provide uncompromising resistance against harsh soil chemistry, corrosion, fresh water, wastewater, crude oils, petroleum fuels, and aggressive industrial chemicals. Backed by rigorous laboratory testing, advanced inspection protocols, and a solid 5-year structural warranty, we deliver safe, leak-proof containment engineered to safeguard your vital infrastructure and the environment for decades.

Engineered Underground Storage Solutions: Advanced Heavy-Duty Containment for Petroleum & Industrial Chemicals
Drawing upon an industrial manufacturing legacy founded in Kuwait in the 1960s, Neama Group delivers specialized, custom-engineered underground fiberglass (FRP/GRP) tanks designed primarily for the safe, long-term containment of petroleum products, aggressive chemicals, and industrial fuels. Manufactured as a seamless, high-strength cylindrical structure in single-wall and double-wall (interstitial monitoring) configurations, our underground systems are built to withstand immense soil compaction, live dynamic traffic loads, and hydrostatic water table pressures without structural deformation.
Engineered under strict international ISO standards, each tank utilizes premium vinyl ester and specialized chemical-resistant resin matrices that provide 100% resistance to internal chemical attack, fuel degradation, external soil acidity, and electrolytic corrosion. Spanning flexible custom capacities from 2,000 liters up to 200,000 liters, Neama underground storage tanks serve commercial petrol stations, chemical manufacturing plants, and heavy industrial facilities with absolute zero-leakage security. Every unit is thoroughly validated using advanced laboratory testing protocols and hydrostatic pressure analysis by our certified engineering team, supported by a 5-year structural warranty for maximum environmental and operational safety.

Expanding upon over sixty years of manufacturing excellence in Kuwait, Neama Group engineers high-integrity fiberglass (FRP / GRP) cylindrical tanks tailored to a diverse spectrum of municipal, agricultural, commercial, and industrial operations. Available in both horizontal and vertical orientations for above-ground and underground installations, these vessels provide an adaptable storage architecture spanning custom volumes from 2,000 to 200,000 liters.
Versatile Operational Capabilities:
- Wastewater & Septic Systems: Built to resist biological fouling, harsh sewage gases (H₂S), and subterranean microbial degradation without requiring interior recoating.
- Potable & Irrigation Water Storage: Formulated with food-grade internal barrier coats that eliminate bacterial growth, prevent algal blooming, and maintain fresh water purity over extended holding periods.
- Industrial & Hazardous Waste Containment: Engineered with specialized thermosetting resin layers capable of handling variable pH ranges, industrial effluents, oils, and chemical byproducts.
- Structural Durability & Quality Assurance: Fabricated with high-strength composite laminates that eliminate external rusting and electrolytic pitting caused by aggressive soils and saline environments.
Every fiberglass tank undergoes rigorous hydrostatic validation, wall-thickness ultrasonic testing, and QA inspection by our engineering specialists under certified ISO standards, backed by a comprehensive 5-year structural manufacturer warranty.
International Accreditations
Certified Global Standards Powering Over Six Decades of Engineering Trust in Kuwait
Since the 1960s, Neama Group has stood as the benchmark for water storage engineering in Kuwait, safeguarding drinking water in over 90% of homes and serving as the trusted partner for major government ministries, municipalities, and mega industrial infrastructure. Our commitment to absolute water safety, long-lasting durability, and superior value is verified by prestigious international accreditations and state-of-the-art laboratory testing:
- ISO 9001:2015: Quality Management System ensuring defect-free manufacturing, uniform rotational molding, and consistent multi-layer barrier thickness.
- ISO 14001:2015: Environmental Management System validating sustainable, eco-friendly industrial practices and zero-leak environmental protection.
- ISO 45001:2018: Occupational Health and Safety Management System governing factory operations and precision assembly standards.
- NSF / ANSI 61 & WRAS Compliance: Certified drinking water safety testing verifying zero toxicity, zero residual styrene, and pure, odorless, and bacteria-free potable water storage year-round.
When you choose Neama, you invest in Kuwait’s most certified water systems, backed by industry-leading warranties of up to 20 years and unrivaled after-sales engineering support.


